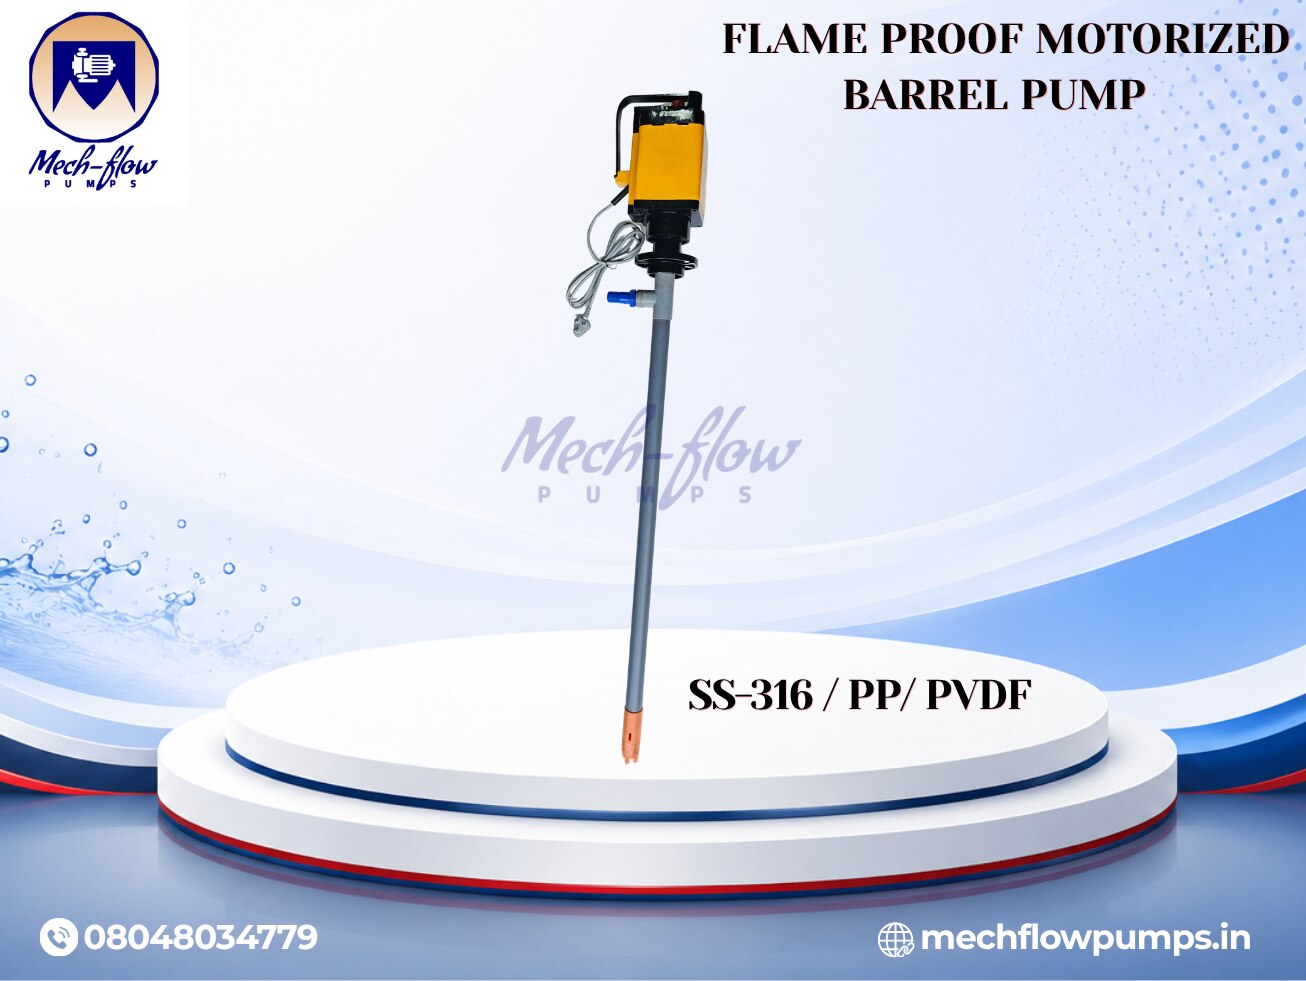
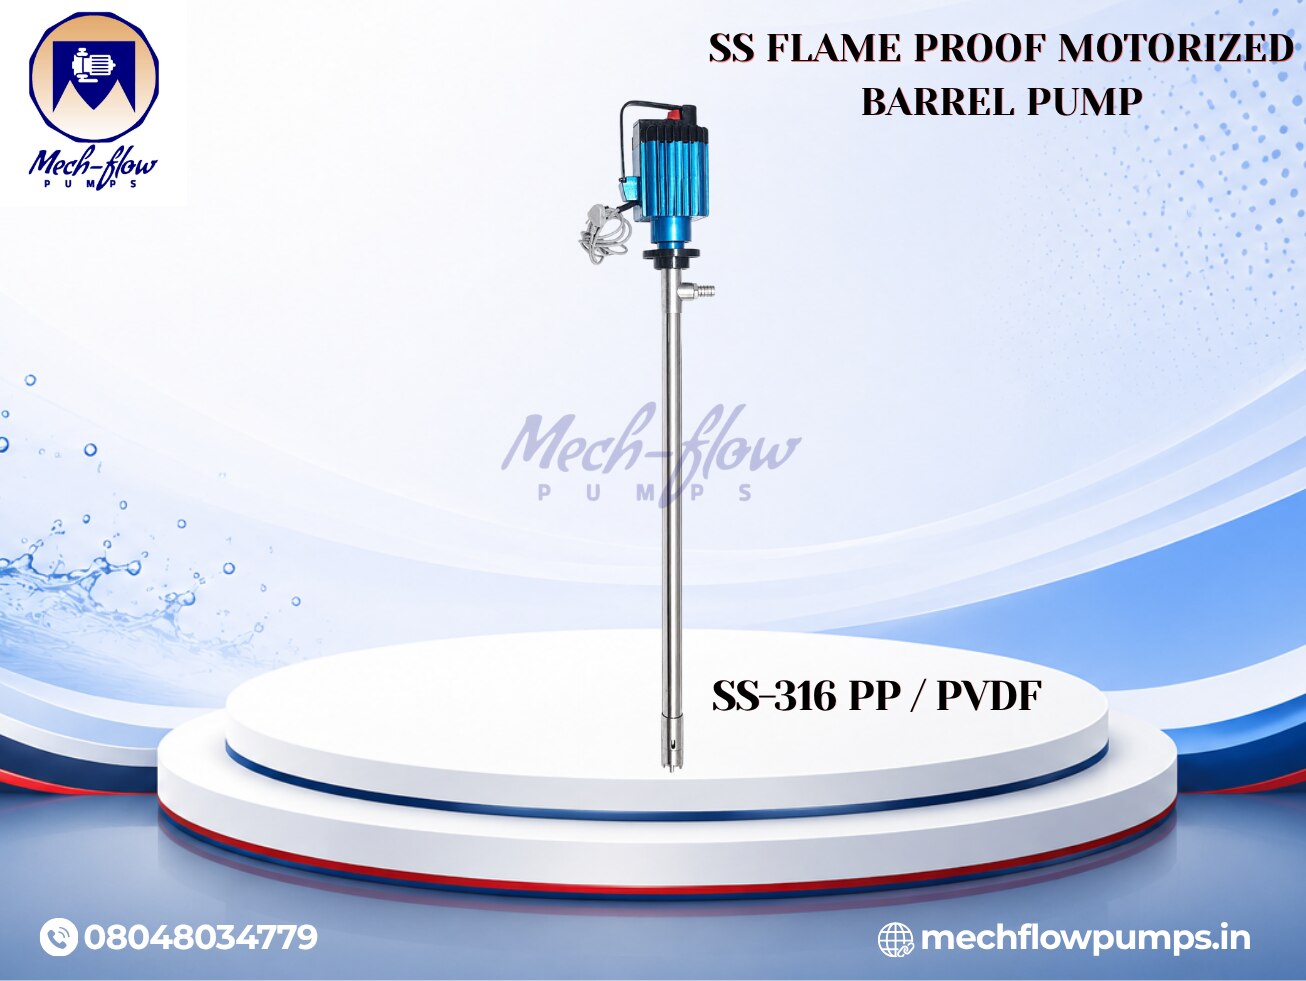
FLAME PROOF MOTORIZED BARREL PUMP
Description
Flame Proof Motorized Barrel Pump Manufacturer in Ahmedabad.
Mech-Flow Pumps is a trusted Manufacturer of Flame-Proof Motorized Barrel Pumps in Ahmedabad, offering safe, efficient, and reliable liquid transfer solutions for industrial applications. Transferring flammable, volatile, corrosive, or hazardous liquids from drums and barrels requires equipment designed to meet strict safety and performance standards. Our robust motorized barrel pumps are engineered to transfer solvents, fuels, chemicals, oils, and other industrial liquids with minimal effort while reducing transfer time and improving workplace safety. Manufactured using high-quality stainless steel and other chemically resistant materials, these pumps deliver excellent durability and dependable performance in demanding environments across the chemical, pharmaceutical, oil, food-processing, and allied industries.
A Flame-Proof Motorized Barrel Pump operates using a vertical immersion tube that is inserted directly into a drum or barrel, allowing efficient liquid transfer without manual lifting or drum tipping. The flame-proof motor configuration makes these pumps suitable for locations where combustible vapors may be present, helping industries maintain safe operations. Depending on the liquid being handled, pump tubes are available in materials such as SS316, PP, and PVDF to ensure optimum chemical compatibility and long service life. As a reliable Flame Proof Motorized Barrel Pumps Supplier in Gujarat, Mech-Flow Pumps provides application-specific solutions tailored to liquid properties, operating conditions, and industry requirements.
Key Features
• Flameproof motor configuration for suitable hazardous-area applications
• Robust SS 316 construction option
• Excellent resistance to corrosion
• Efficient liquid transfer from drums and barrels
• Compact and portable design
• Easy insertion and removal from containers
• Simple operation and maintenance
• Suitable for continuous-duty applications when correctly specified
• Different immersion tube materials available
• Suitable for a wide range of industrial liquids
• Reliable performance in demanding working environments
• Anti-static grounding arrangements can be provided where required.
Applications
Flame-Proof Motorized Barrel Pumps are commonly used for:
• Barrel and drum unloading
• Solvent transfer
• Chemical transfer
• Pharmaceutical liquid handling
• Paint and coating industries
• Oil and lubricant transfer
• Petroleum product handling
• Food and beverage liquid transfer
• Industrial fluid transfer
• Process chemical dosing and transfer
As an established Flame Proof Motorized Barrel Pumps Distributor in India, Mech-Flow Pumps serves diverse industrial applications with practical and application-specific pumping solutions.
Suitable Liquids
Our Flame Proof Motorized Barrel Pumps are suitable for transferring a wide range of low-viscosity liquids, including industrial chemicals, solvents, IPA and alcohol-based liquids, mild acids and alkalis, oils, lubricants, diesel, selected petroleum products, pharmaceutical liquids, food-grade liquids, and other industrial fluids. To ensure safe, reliable, and efficient operation, the pump material, seal type, flame-proof motor certification, grounding system, and hose arrangement should always be selected according to the specific liquid being handled and the applicable hazardous-area classification.
Construction & Material Options
• Pump Tube: SS 316 / PP / PVDF, depending on application
• Motor: Flameproof motor option
• Drive: Motor-driven pumping arrangement
• Wetted Components: Selected according to chemical compatibility
• Grounding: Anti-static grounding provisions available where required
• Design: Modular construction for convenient handling and servicing
Why Choose Mech-Flow Pumps?
Mech-Flow Pumps combines practical engineering, dependable construction, and application-specific expertise to deliver safe and efficient liquid transfer solutions. As a trusted Flame Proof Motorized Barrel Pumps Wholesaler in Gujarat, we provide high-quality pumps tailored to the requirements of various industrial applications. Our experienced team works closely with customers to recommend the most suitable pump tube materials, motor configurations, seals, hoses, and accessories based on the type of liquid being handled and the operating environment, ensuring reliable performance, enhanced safety, and long-term operational efficiency.
Frequently Asked Questions
1. What are Flame Proof Motorized Barrel Pumps used for?
They are designed for transferring liquids from drums, barrels, and containers, particularly where flammable or volatile liquids require appropriately certified motor equipment.
2. Which materials are available for barrel pump tubes?
Depending on chemical compatibility, pump tubes can be supplied in SS 316, PP, or PVDF construction.
3. Why choose Mech-Flow Pumps?
Mech-Flow Pumps is a trusted Flame Proof Motorized Barrel Pumps Manufacturer in Ahmedabad, providing reliable industrial transfer pumps, application-based material selection, and technical support.
Need safe drum-to-process liquid transfer? Contact Mech-Flow Pumps for the right Flame Proof Motorized Barrel Pump for your application.